Introduction
Treat a production G-code file like a stray Word document, and you're one careless edit away from a scrapped part or a machine crash.
A Modern Machine Shop review of common CNC programming mistakes found that errors don't always trigger an alarm. They just cause confusion, wasted cycle time, or scrap, often because operators can't tell which revision they're actually running.
This article covers four activities that often get lumped together under "editing G-code":
- Inspecting and modifying a posted program
- Validating tool motion before it runs
- Getting engineering sign-off on the change
- Moving only the approved file through a controlled transfer to the machine
Skip any one of these steps, and the other three don't count for much.
We'll walk through what a proper G-code editor should do, how to build an edit-and-approval workflow, and how version control keeps outdated files off the shop floor.
Key Takeaways
- A G-code editor supports review and targeted edits—but it doesn't replace CAM verification, simulation, or safe operating procedures.
- Every manual edit needs a documented reason, a reviewer, a revision ID, and a validation record before release.
- Working files and approved files should never share a folder; filenames alone can't prove approval status.
- DNC and shop-floor systems should deliver the released revision automatically, without skipping human review.
What a G-code Editor Does in a CNC Programming Workflow
A G-code editor sits at a specific point in the programming sequence, not at the start of it. CAM software builds toolpaths from a 3D model; a post-processor translates those toolpaths into the G-code and M-code your specific controller understands. The editor is where someone inspects that output, makes a justified change if needed, and validates the result before it reaches the machine. That distinction matters because G-code itself is just controller-facing instructions. The NIST RS274NGC interpreter documentation describes it plainly: programs are made of line-based blocks, blocks contain words, and each word pairs a letter, mostly G or M, with a number. Nothing in that structure tells you whether the code is correct for your part.

Core Functions to Look For
A capable editor should give reviewers:
- Syntax-aware viewing: line numbers, block navigation, search and find/replace across the whole file or a selected block
- Visibility into program structure: headers, tool calls, offsets, coordinate systems, feeds and speeds, and program endings
- Backplotting or simulation: a way to connect a line of code to the physical motion it produces Machine Link™, for example, lets a programmer open a posted file and use Search and Replace for speed and feed adjustments across an entire program or just a selected block, then save that edit under a new file name. That's useful for quick, targeted changes, but it's not a substitute for confirming the change is correct.
Why Controller Compatibility Still Matters
G-code follows broad conventions, but dialects vary widely. Haas controls use G54/G55 for work offsets and G81/G83 for drilling canned cycles; Siemens SINUMERIK controls call cycles like CYCLE74 or CYCLE75 with entirely different parameter syntax. An edit that works cleanly on one controller can throw an alarm on another, or worse, run silently wrong. Some edits belong in the CAM file, not the editor. Send these back through CAM and repost:
- Geometry or sequencing changes
- New coordinate strategies
- Cutting-condition overhauls The editor is for smaller, documented corrections, not general-purpose find-and-replace. Keep the original posted file untouched, record exactly what changed, and validate before anything moves toward the machine.
A Safe Edit-and-Approval Workflow Before Machine Transfer
A repeatable workflow needs clear ownership at each step. Use this sequence every time a program moves toward the machine:
- Identify the job and machine
- Load the correct program
- Inspect it
- Make the smallest justified edit
- Validate that edit
- Submit it for approval
- Release only the approved revision
Review Before You Touch Anything
Before editing, confirm:
- Part number, job or work order, material, target machine, and controller
- Post-processor used and units (inch vs. metric)
- Work offset strategy and intended setup
- That the file came from the intended CAM operation, not an obsolete copy pulled from a local machine or a shared folder
Snavely's Machine runs more than 30 CNC machine tools across 10 different control types. Their team has seen the same gap: getting the right program to the right machine, on the right control, isn't automatic just because a file exists somewhere on the network.
Making the Edit
Document each change before you move on:
- Why the edit happened
- Which blocks changed
- Who made it
- What setup information might be affected downstream
A short in-code comment—such as STOP POSITION ABOVE TT PLATE or DRILL TO DEPTH—helps the next person understand intent without guessing.
Do not edit without review: safety lines, tool-change logic, offsets, macros, or probing routines. These blocks interact with the machine's physical state in ways that aren't obvious from reading code alone. Keep a read-only baseline of the original export so you can always compare or restore.
Validating the Result
After you edit, don't assume the program is correct:
- Run a syntax or controller-compatibility check if your editor supports one.
- Backplot or simulate to review travel direction, rapid moves, tool changes, offsets, and spindle behavior.
- Compare against the prior approved revision to confirm unrelated blocks weren't touched.
The NIMS machine verification and dry run standard lists this exact kind of check: proving an unproven program without cutting production parts, setting offsets, evaluating collision risk, and confirming the program stays inside travel limits.
The Approval Gate
Require the programmer to explain the change. Have a reviewer check it against the drawing, setup sheet, tooling, and machine requirements. Record:
- Approval status
- Reviewer name and date
- Revision number
- Any special setup notes
Once approved, move the file into a controlled release location where it can't be accidentally overwritten. At the machine, the operator should confirm they're running the released revision before hitting cycle start.

Version Control for CNC Programs: Revisions, Permissions, and Traceability
A filename like "final," "final2," or "latest" doesn't show ownership, approval status, or history. None of those names tell you who approved the file, when, or what changed since the last run.
A Practical Program Lifecycle
Every CNC program should move through defined states:
| Stage | Meaning |
|---|---|
| Working/draft | Editable by authorized programmers; not approved for production |
| Review | Awaiting technical, manufacturing, quality, or customer checks |
| Released | Approved for a defined machine, controller, and setup |
| Obsolete/superseded | Kept for traceability, blocked from routine transfer |
Each revision should carry metadata such as:
- Part and operation identifiers
- Machine/controller and program revision number
- Source CAM file or post-processor
- Author, change reason, reviewer, and approval date
- Links to related setup documentation
Reducing the Chance of Running an Outdated File
- Restrict who can edit, approve, release, overwrite, or delete programs
- Use read-only permissions or a controlled repository for released files
- Display revision and release status in the program header and in whatever system transfers the file
This is where basic file management tools show their limits. Mike Hamonds of M-Tech Machine Products has noted that Machine Link™ keeps CNC files safely stored on the shop computer, which solves part of the problem. But storage isn't version control.
Directory listings show file name, size, and last modification date—not who approved a revision or why it changed. If your shop needs a documented approval trail, build it into the process around the editor rather than assuming it from a timestamp.
Comparing and Rolling Back
Use a text or manufacturing-aware comparison tool to identify exactly which blocks changed, separating real edits from formatting noise. Keep every prior approved version. When a defect shows up three weeks later, you need to reproduce the run that made it, or fall back to a known-good program while you investigate.

ISO 9001's documented information requirements still apply here in spirit, even for shops not pursuing certification. Information should be controlled, retained, and available as evidence that a process ran as planned. Whether that control lives in a document-management system, a PLM tool, an MES, or your DNC platform depends on what that specific tool actually verifies. Check its real revision and audit capabilities before relying on it.
What to Check Before the Program Hits the Machine
A code review isn't the same as a physical setup check. Both need to happen before the cycle starts.
Pre-Release Checklist
Before any program reaches a machine, confirm:
- Program identity and revision number
- Target machine and controller
- Units (inch/metric) and coordinate system
- Work offsets and tool numbers, lengths, and diameters
- Feeds, speeds, and spindle direction
- Coolant calls, probing routines, safe-start blocks, and program end
Code Review vs. Physical Setup
Reviewing code on screen confirms the logic is sound. It doesn't confirm that the actual tools, holders, fixtures, stock, work offsets, and clamps on the machine match what the program expects. Both checks are required—neither replaces the other.
Staged Verification at the Machine
A reasonable staged approach, adjusted to your shop's own procedures:
- Confirm file identity and successful transfer.
- Run in graphics or simulation mode.
- Step through in single-block or reduced-feed mode.
- Complete a dry run.
- Inspect the first piece.
Haas operator manuals describe GRAPHICS mode for no-motion verification and SINGLE BLOCK for one-block-at-a-time execution. Both are standard tools at this stage. Your machine manufacturer's guidance and your site's safety rules always take precedence over any general checklist, including this one.
Connecting the G-code Editor to Shop-Floor Systems
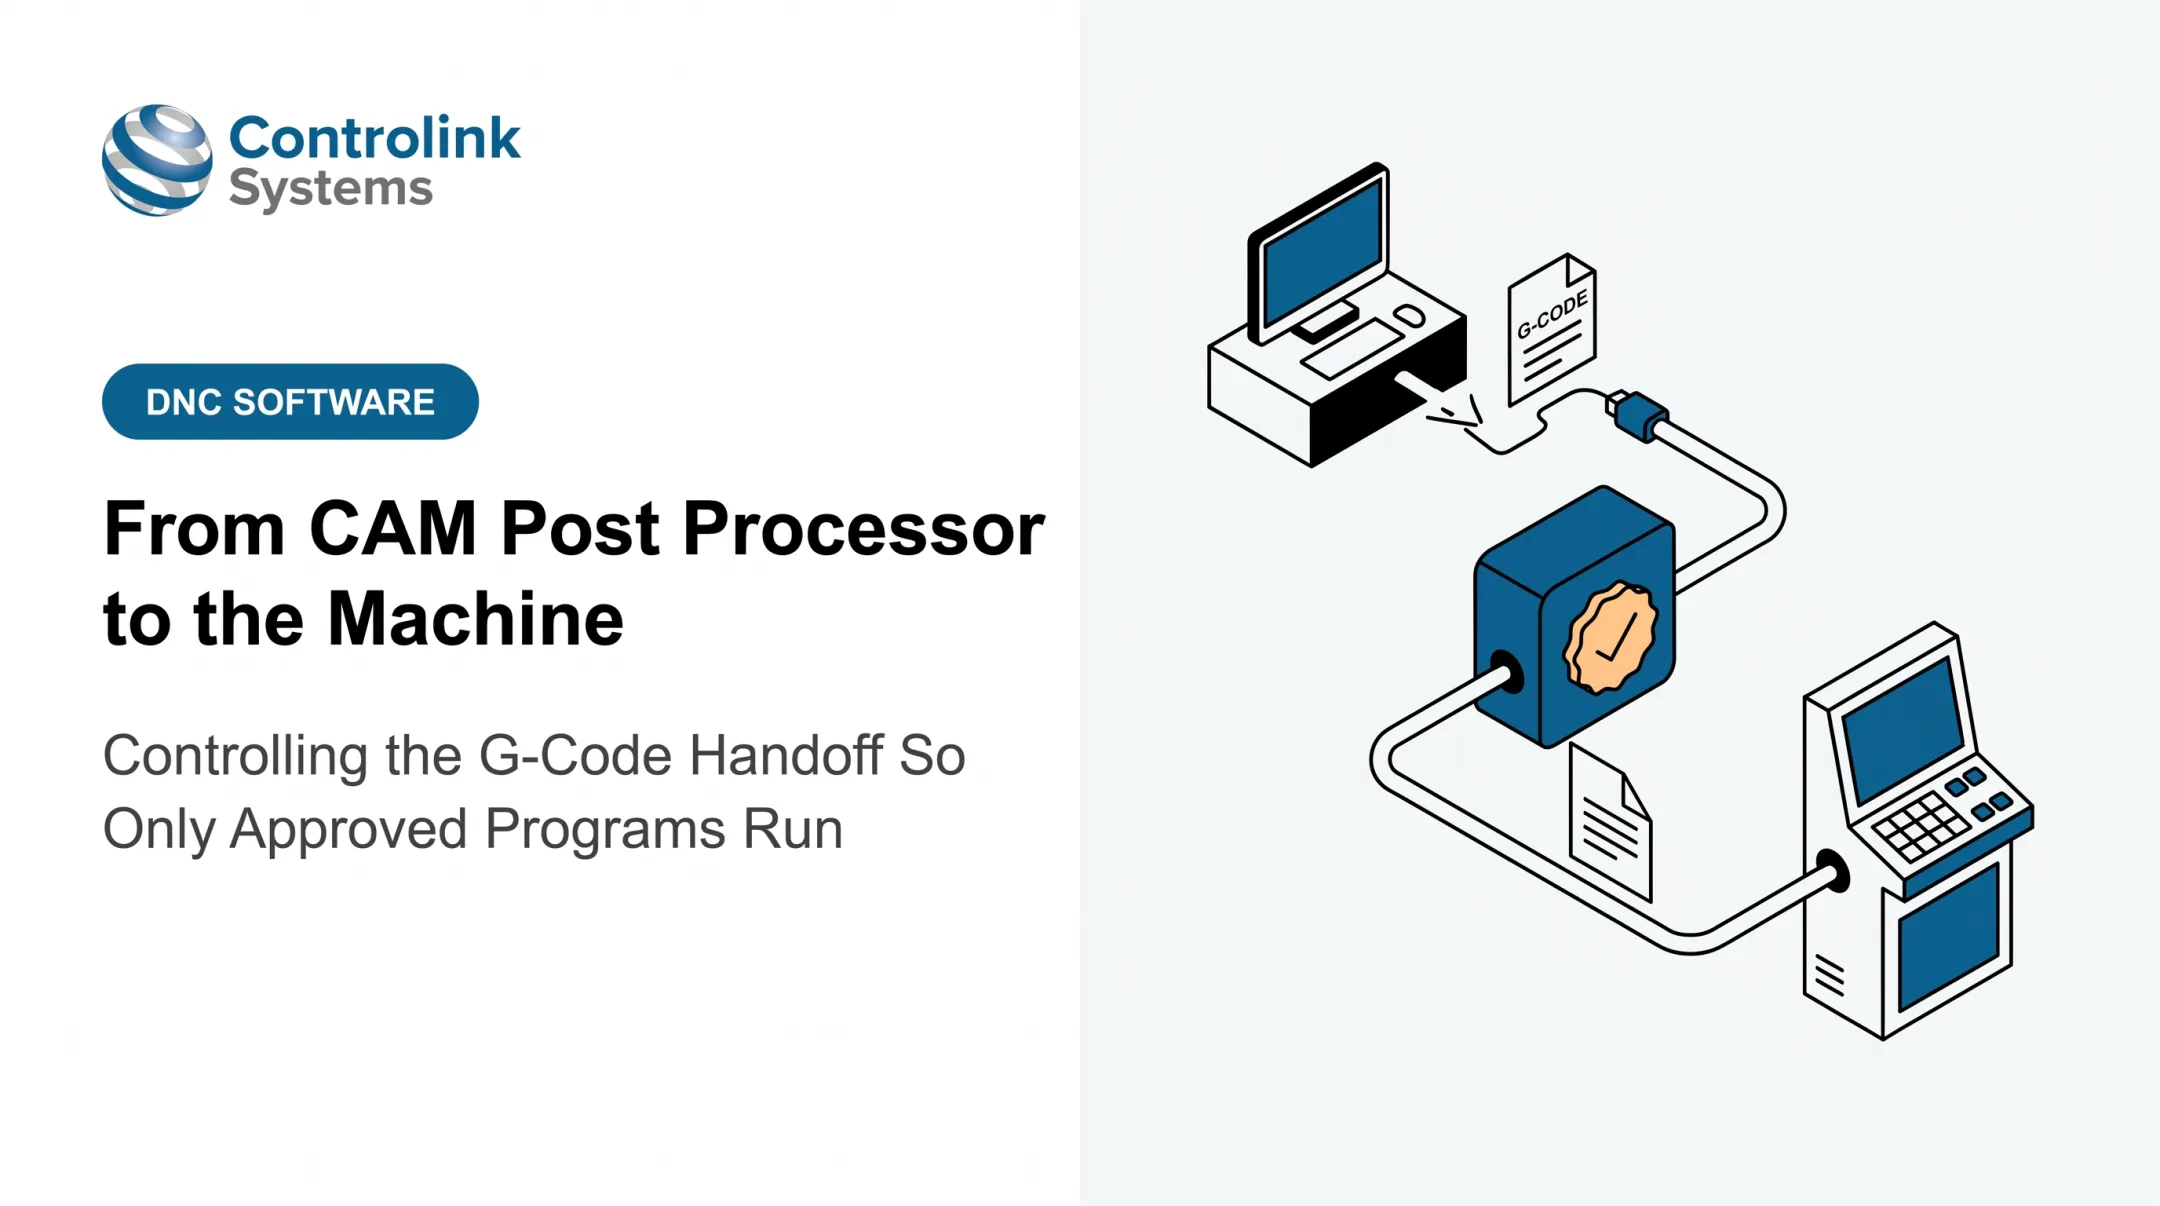
An editor and approval process only prevents outdated-file problems if the approved file reaches the machine without a detour. That's where CNC/DNC communication and shop-floor automation come in, connecting the editor's output to shared repositories, machine controls, and whatever software operators use at the console.

Questions Worth Researching First
Before selecting a connected solution, ask:
- Which controllers and communication protocols are supported?
- How does the system identify which machine is requesting a file?
- Who has permission to release, request, or overwrite files?
- Is revision status visible to the operator before transfer?
- Does the system log transfers, and how does it behave offline?
- Does it fit with your existing CAM and manufacturing systems?
Where Controlink Fits
At fleet scale, manual file-hunting stops being practical. Richard Recker of Busche Enterprises has described backing up CNC programs across 46 machine tools—the point where a connected system starts paying for itself.
Controlink Systems LLC has built CNC/DNC communication and shop-floor automation software since 1998, and has been part of the NI Partner Network since 2000. Relevant products include:
- Machine Link™ — file editing and RS-232 transfer to and from the control
- QUICK Serve — automated file requests across fleets from 3 to 64 machines, so operators pull the file assigned to their machine instead of grabbing whatever sits in a shared folder
- PDADNC™ — similar file handling, including drip feeding, for shops on standard ASCII, ISO, or EIA controls
If you need to keep outdated files off the machine, evaluate whether one integrated path—editor, transfer method, and approval—matches your controllers and workflow.
Automation Should Never Skip the Human Step
No matter how a system moves files, it shouldn't move around the approval gate. Automatic transfer needs to preserve revision review, setup verification, and operator confirmation, not bypass them for the sake of speed. The goal is getting the correct file to the machine faster, not just any file.
Frequently Asked Questions
Is G-code still relevant today?
Yes. G-code remains the controller-facing language driving most CNC machines, even as CAM, simulation, DNC, and shop-floor automation tools change how those programs get created, checked, and delivered.
What is a G-code editor used for?
A G-code editor is used to inspect a posted program, make targeted edits with search/replace, review tool calls and offsets, backplot or simulate motion, and save a validated file for the correct controller.
Can you safely edit G-code manually?
Yes, for limited, documented changes that get validated before release. Geometry, sequencing, or cutting-condition changes should generally go back through CAM and get reposted instead.
How should CNC programs be version-controlled?
Assign each revision a unique identifier, separate working files from released files, restrict who can approve or overwrite programs, and keep every superseded version for traceability.
What should be checked before sending G-code to a CNC machine?
Confirm controller compatibility, units, offsets, tools, feeds and speeds, workholding, and safe moves. Then simulate or dry-run and verify you're running the current approved revision.